Minimal Space. Maximum Impact! Designed for when every millimeter matters> the new IRONLESS UNANO SERIES
Semiconductors
Increase throughput and precision of your system
Display
Enhance accuracy and precision with linear motors
Science and aerospace
Improve motion quality for a variety of applications
Machine tooling
Robust solutions for increased speed and precision
Digital cutting
Create modular and high throughput applications
Printing
Increase printing speed and quality using linear motors
Robotics
Integrate compact solutions for guaranteed uptime and high dynamics
Life science
Establish precise and clean integrated solutions
Woodworking
Maximize performance and accuracy for high throughput
Stages and system solutions
Compact integration and high performance for your axis
Vacuum applications
Best performance for clean and vacuum applications
Characteristics
Choosing the right Industrial Foiling Machine can shape product quality, production speed, and long-term operating costs. In packaging plants, the decision becomes visible in small details. Foil must cover sharp letters evenly. Fine lines should remain clean. Adhesion must survive handling, transport, and shelf display.
Dr. Sean Smyth, a respected print-industry consultant, highlights a practical principle: “Consistent quality depends on process control, not the machine alone.” This view matters when comparing an Industrial Foiling Machine manufacturer. A reliable supplier should explain heating systems, foil tension control, pressure adjustment, registration accuracy, and maintenance access. Technical claims are not enough. Buyers need test samples, measurable tolerances, and clear service commitments.
A strong machine should match the real production environment. A narrow web may require different controls from a wide-sheet system. Short runs may reward quick setup. Long runs demand stable temperature and repeatable feeding. Operators also need accessible controls and safe working procedures. Small improvements matter.
Still, no machine removes every production challenge. Material changes can affect adhesion. Humidity may influence paper behavior. Inexperienced setup can create waste, even with advanced equipment. That is why trustworthy manufacturers provide commissioning support, operator training, spare parts, and documented testing.
This guide examines China’s Industrial Foiling Machine manufacturing sector through practical performance, engineering capability, customization, quality assurance, and after-sales support. The goal is not to promote the most impressive specification sheet. It is to identify equipment that performs consistently beside a real production line, shift after shift.
Industrial Foiling Machines: Definition and Core Functions
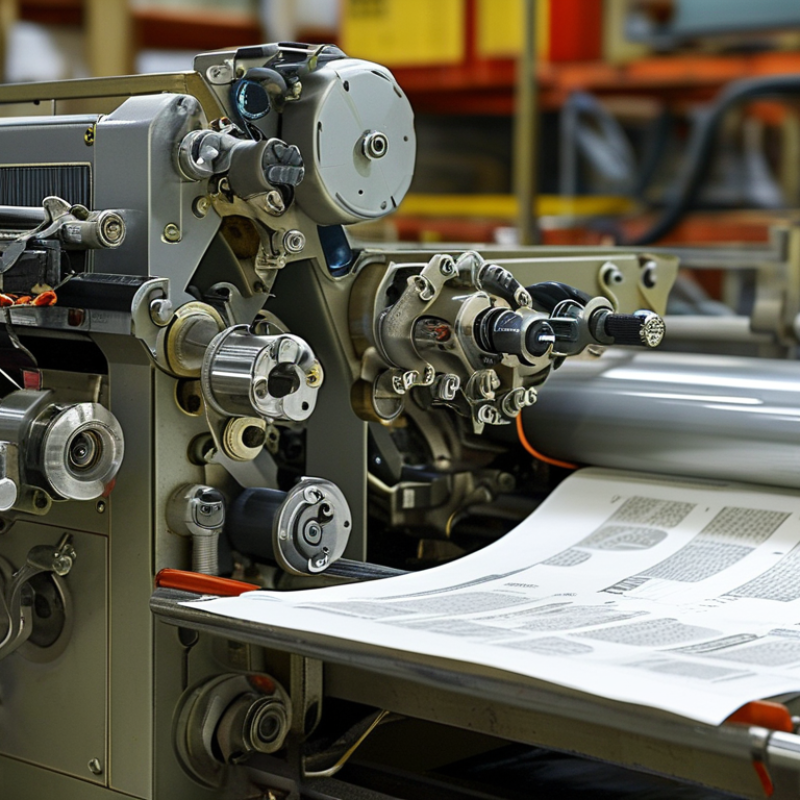
An industrial foiling machine applies metallic or colored foil to paper, cartons, labels, plastics, and selected coated materials. It uses controlled heat, pressure, and a patterned die to transfer the foil accurately. In production, the machine usually includes a feeding system, heating unit, foil unwinding shaft, stamping cylinder, pressure mechanism, and waste-rewinding section. These parts must work together. A weak setting can create dull patches, wrinkles, or incomplete transfer.
Its core functions include hot foil stamping, precise material feeding, foil tension control, registration adjustment, and production-speed management. Advanced systems may support multiple foil rolls, automatic temperature control, and sensor-based alignment. Operators often adjust pressure according to substrate thickness and surface coating. Excessive heat may damage sensitive stock. Low pressure may leave broken lettering. From practical testing, the first setting is rarely perfect, especially with recycled or uneven materials. That detail is easy to underestimate.
Tips: Check the substrate before production. Run a short sample and inspect fine lines, corners, and solid areas. Keep the die clean and monitor foil tension during long runs. Record temperature, pressure, and speed for repeat orders. This simple record improves reliability, although it will not replace skilled judgment. A careful operator still needs to watch the machine, listen for unusual movement, and stop early when results begin changing.
Industrial foiling equipment now depends on more than pressure and heat. Servo-driven web handling keeps foil tension stable during high-speed production. Closed-loop controls adjust unwinding, rewinding, and registration continuously. Small deviations matter.
A 2024 Grand View Research estimate places the global hot stamping foil market at more than USD 1 billion, with steady growth expected through 2030. This expansion increases demand for precise thermal systems. Ceramic or infrared heaters can shorten warm-up time and improve temperature uniformity. Yet, excessive heat can distort thin films or weaken adhesive layers. Careful testing remains essential.
Modern machines also use optical sensors, PLC automation, and inline inspection cameras. These systems detect missing impressions, wrinkles, and registration errors before waste increases. Smithers reported that the global print market remains worth hundreds of billions of dollars, while productivity and material efficiency continue gaining importance. That pressure is visible on factory floors. Less scrap. Faster changeovers.
In practice, one setting rarely fits every substrate. Paper, plastic film, and coated board respond differently. Experienced operators still adjust pressure, dwell time, and foil tension by observing the actual impression. A perfect specification sheet can fail beside a humid production line. Energy monitoring, quick-clean components, and remote diagnostics can improve reliability, but maintenance discipline is still uneven. This is where equipment design needs more honest evaluation.
| Technology or System | Operating Principle | Typical Industrial Parameters | Suitable Materials and Applications | Main Advantages | Important Control Factors |
|---|---|---|---|---|---|
| Hot Foil Stamping | A heated die or stamping plate activates the adhesive layer of a foil and transfers the metallic or pigmented layer onto the substrate under pressure. | Foil activation temperature: commonly about 90–180°C Pressure: adjusted according to substrate, die area, and foil type Process speed: machine- and material-dependent | Paperboard, coated paper, labels, plastics, synthetic films, packaging, security print, and decorative graphics. | High opacity, strong metallic appearance, precise solid areas, and compatibility with embossed or raised effects. | Die temperature, dwell time, pressure balance, foil release characteristics, substrate coating, and registration accuracy. |
| Cold Foil Transfer | An adhesive is printed onto selected areas of the substrate. Foil is laminated to the adhesive and the carrier film is removed after transfer. | No heated stamping die is normally required Adhesive curing may use UV or LED-UV systems Suitable for continuous web production | Paper, folding cartons, pressure-sensitive labels, flexible packaging, and printed decorative effects. | Efficient inline integration, fine image detail, lower thermal load, and good compatibility with high-speed printing workflows. | Adhesive coat weight, curing energy, nip pressure, web tension, foil release, ink compatibility, and surface cleanliness. |
| Digital Foiling | A digitally controlled toner, ink, or adhesive image selectively receives foil without using a conventional engraved stamping die. | Variable-data capability: supported Setup time: generally lower than die-based processes Production speed: dependent on digital engine and substrate | Short-run packaging, personalized labels, prototypes, promotional print, and variable-data graphics. | Fast changeovers, no physical die storage, economical short runs, and personalization of each printed sheet or web section. | Surface energy, toner or adhesive formulation, foil compatibility, fusing conditions, image density, and substrate flatness. |
| Rotary Foiling | A cylindrical engraved or etched tool continuously transfers foil as the web or sheet passes through a rotary nip. | Continuous web or sheet-fed operation Register controlled by encoder and servo feedback Speed limited by substrate, foil, tooling, and drying conditions | Labels, narrow-web packaging, decorative films, flexible materials, and high-volume printed products. | Continuous production, consistent repeat quality, reduced intermittent motion, and good suitability for inline processing. | Rotary tool circumference, nip pressure, web tension, phase synchronization, anilox or adhesive delivery, and waste control. |
| Sheet-Fed Foiling | Individual sheets are registered and transported through a stamping or transfer unit for controlled foil application. | Sheet registration generally controlled by front lays and side lays Suitable for rigid sheets and board stocks Processing speed depends on sheet size, coverage, and machine format | Cartons, book covers, greeting cards, certificates, commercial print, and premium paper products. | Accurate sheet handling, strong suitability for heavy substrates, and flexible job-to-job production. | Sheet squareness, gripper condition, static electricity, make-ready settings, die pressure distribution, and waste stripping. |
| Web Tension Control | Load cells, dancer rollers, or torque-controlled drives maintain stable tension throughout unwinding, processing, and rewinding. | Closed-loop control commonly uses load-cell feedback Tension setpoint varies with substrate width, thickness, and winding diameter Low tension helps reduce stretching and registration errors | Paper webs, plastic films, label stock, laminates, and other continuous-roll materials. | Improves dimensional stability, foil tracking, print-to-foil registration, and finished-roll quality. | Unwind brake response, roll hardness, splice quality, humidity, material elongation, and acceleration profiles. |
| Servo Registration and Drive Synchronization | Servo motors and electronic gearing synchronize the foil feed, substrate movement, printing unit, and stamping cylinder. | Encoder-based position feedback Electronic phase adjustment during production Register performance depends on substrate stability and control resolution | Multicolor packaging, labels, precise graphics, holographic effects, and inline converting processes. | Accurate repeat positioning, faster changeovers, reduced setup waste, and improved consistency at variable speeds. | Encoder calibration, web slip, mechanical backlash, acceleration control, registration marks, and control-loop tuning. |
| Foil Unwinding and Rewinding | Controlled unwind and rewind systems feed foil at a stable rate while maintaining suitable roll tension and alignment. | Supports roll-to-roll foil handling Pneumatic or mechanical shaft options may be used Edge guiding can correct lateral drift | Metalized polyester foils, pigment foils, holographic foils, transparent foils, and specialty decorative films. | Stable foil delivery, reduced wrinkles, improved utilization, and reliable long-run operation. | Core size, roll diameter, brake torque, web alignment, splice quality, foil curl, and lateral tracking. |
| Heating and Temperature Management | Heating elements and temperature sensors maintain the die, roller, or transfer surface within a selected process range. | Typical controlled range: approximately 90–180°C for many hot-stamping applications Actual setting depends on foil, substrate, tooling, and machine design Closed-loop PID control is commonly used | Hot-stamping foils, coated papers, boards, films, plastics, and heat-sensitive decorative substrates. | More consistent foil release, stable image quality, and reduced defects caused by temperature fluctuation. | Sensor location, heater response, thermal uniformity, ambient conditions, dwell time, and machine warm-up procedure. |
| Pressure and Nip Control | Mechanical or servo-controlled pressure brings the foil, substrate, adhesive, and tooling into uniform contact. | Pressure is selected by product and coverage area rather than one universal value Pneumatic, hydraulic, mechanical, or servo actuation may be used Uniformity across the working width is essential | Solid foil areas, fine text, line work, embossed graphics, laminated products, and coated substrates. | Supports clear transfer, minimizes incomplete coverage, and reduces substrate deformation when correctly adjusted. | Tool flatness, parallelism, substrate thickness, pressure distribution, dwell time, and machine frame rigidity. |
| Inline Inspection and Defect Monitoring | Cameras, sensors, or stroboscopic systems detect registration errors, missing foil, wrinkles, contamination, and surface defects. | Inspection may be continuous or sampling-based Detection capability depends on camera resolution, contrast, speed, and lighting Defect data can be linked to production length or sheet position | Security print, pharmaceutical packaging, labels, premium cartons, and products requiring traceable quality control. | Early defect detection, lower material waste, improved consistency, and documented production quality. | Lighting stability, inspection threshold, camera focus, dust control, reference pattern quality, and system calibration. |
| Energy-Efficient Heating and Curing | Insulated heating zones, rapid-response heaters, infrared systems, or UV/LED-UV curing systems deliver energy only where the process requires it. | LED-UV systems generally consume energy only during active curing Heating efficiency depends on insulation, control accuracy, and thermal mass Curing dose must match adhesive and ink requirements | Cold foil adhesives, UV inks, hot-stamping tools, coated papers, films, and inline printing-converting systems. | Reduced warm-up time, lower heat exposure, more stable processing, and potential reductions in energy consumption. | Radiant heat management, lamp or LED condition, curing dose, ventilation, substrate sensitivity, and maintenance intervals. |
| Safety and Machine Monitoring | Guard switches, emergency stops, temperature alarms, pressure monitoring, and overload protection reduce operational risks. | Safety systems are designed according to applicable machinery regulations Alarm history and interlock status can be displayed through an HMI Preventive maintenance intervals should be documented | All industrial foiling equipment, including sheet-fed, web-fed, rotary, and inline systems. | Protects operators, reduces unplanned downtime, and supports controlled commissioning and maintenance. | Guarding, lockout procedures, emergency-stop testing, electrical inspection, pneumatic integrity, and operator training. |
Evaluating a foiling machine manufacturer in China requires more than comparing prices. Inspect the factory, not only the showroom. Ask to see machines running with your actual foil, substrate, speed, and design. A reliable manufacturer should explain heating zones, pressure control, web tension, and registration accuracy in practical terms.
Request a detailed test report. It should include temperature stability, operating speed, foil waste, noise, and rejected samples. Ask whether key components have traceable sources and whether electrical systems meet your destination market’s requirements. Clear drawings, installation procedures, and spare-parts lists show professional engineering. Vague answers deserve caution.
Small details matter.
Speak with the technical team, not only sales staff. Their response to a difficult question reveals experience. Confirm remote support hours, response times, training, and warranty conditions in writing. Ask how quickly common parts can be shipped and who pays for service visits. A factory may promise impressive output, yet your material could behave differently during continuous production.
I would also review several customer references and inspect long-term operating records. Photos are useful, but they are not proof. One weakness in my own evaluation was trusting a polished demonstration too quickly. A slower test with real production settings would have exposed alignment drift earlier. Leave room for uncertainty, and ask the manufacturer to document how problems will be corrected.
China Best Industrial Foiling Machine Manufacturer
Manufacturing Standards, Customization, and Quality Control
An experienced industrial foiling machine manufacturer starts with measurable standards, not attractive promises. Production teams inspect steel frames, heating systems, rollers, and electrical cabinets against approved drawings. Critical dimensions are recorded with calibrated tools. Welding seams receive visual checks before painting. This prevents alignment errors from causing unstable feeding or uneven foil transfer. Operators test temperature control, pressure balance, and emergency stopping functions during assembly. Safety matters.
Customization begins with the material, not a standard catalog. Foil width, substrate thickness, working speed, pattern accuracy, and floor space shape the machine design. Engineers may adjust roller hardness, heating zones, control interfaces, or unwinding systems. A factory should confirm these choices through samples and production data. I have found that short trials reveal problems hidden by drawings. Occasionally, the first configuration is not ideal. That is useful evidence.
Quality control continues after final assembly. Each machine needs a documented run test, including start-up time, temperature stability, pressure consistency, noise, and output inspection. Serial records make replacement parts and service decisions more reliable. Skilled technicians photograph key settings and train operators on cleaning and adjustment. Yet inspection is never perfect. Dust, operator habits, and changing materials affect results. Honest manufacturers leave room for correction and keep testing.
Global ISO management-system certificate data provides a useful reference for evaluating manufacturing maturity. ISO 9001 focuses on quality management, while ISO 14001, ISO 45001, and ISO 50001 address environmental, occupational safety, and energy-management controls. For customized industrial foiling equipment, these standards support documented specifications, process validation, inspection records, and continuous quality improvement.
Source: ISO Survey 2022, International Organization for Standardization. Values represent worldwide valid certificates.
Industrial foiling machines serve packaging, labels, folding cartons, book covers, and decorative print work. They apply metallic or pigment foil through controlled heat, pressure, and timing. In production, foil adhesion depends on substrate coating, ink curing, temperature, and machine speed. A stable machine should deliver sharp edges, even coverage, and limited material waste. Operators should test actual materials before approving regular production.
Maintenance is practical, not optional. Clean the foil path daily, especially around rollers and sensors. Check pneumatic pressure, heating plates, bearings, and electrical connections weekly. Record temperature settings, pressure changes, and unusual noise. Small records often reveal faults early. I have seen operators blame the foil when an uneven roller caused the defect. That assumption can waste hours. No machine is perfect.
Tips: Ask the manufacturer for sample results, operating videos, service response times, and maintenance instructions. Confirm working width, maximum speed, compatible substrates, foil types, power requirements, and safety controls. Request a factory acceptance test using your own materials. Compare total ownership costs, not only the purchase price. A lower quote may hide difficult setup, spare-part delays, or limited technical training. Speak with experienced users when possible, and question impressive claims that lack measurable test data.